Data Collection
Every bolt. Every pull. Documented.
A crucial advantage of AutoBolt: all data is collected automatically, without human intervention. For every bolt you get a time-stamped, tamper-free record — uploaded to a Data Cloud and turned into reports.
Collected automatically
The robot records every value itself while it works. No manual writing, no typing errors, no human intervention.
Tamper-free
Data is stored in tamper-free files directly from the AutoBolt control system — a trustworthy quality record.
Data Cloud
Data is uploaded to a Data Cloud for big-data analysis across flanges, turbines and campaigns.
Reports generated
Controlled quality reports are produced per flange and per campaign, ready for the client and QA/QC.
What is recorded for each bolt
- Time stamp
- Exact date and time of every pull on every bolt.
- Hydraulic pressure
- Applied pressure measured on two independent sensor channels.
- Turn of the nut
- Nut rotation in degrees, per pull, on both channels.
- Number of pulls
- Every pull is logged — first-pull acceptance or re-tightening.
- Residual torque
- Torque applied to the nut after tensioning.
- Tool & pump traceability
- Which elongation tool and hydraulic pump were used for each bolt.
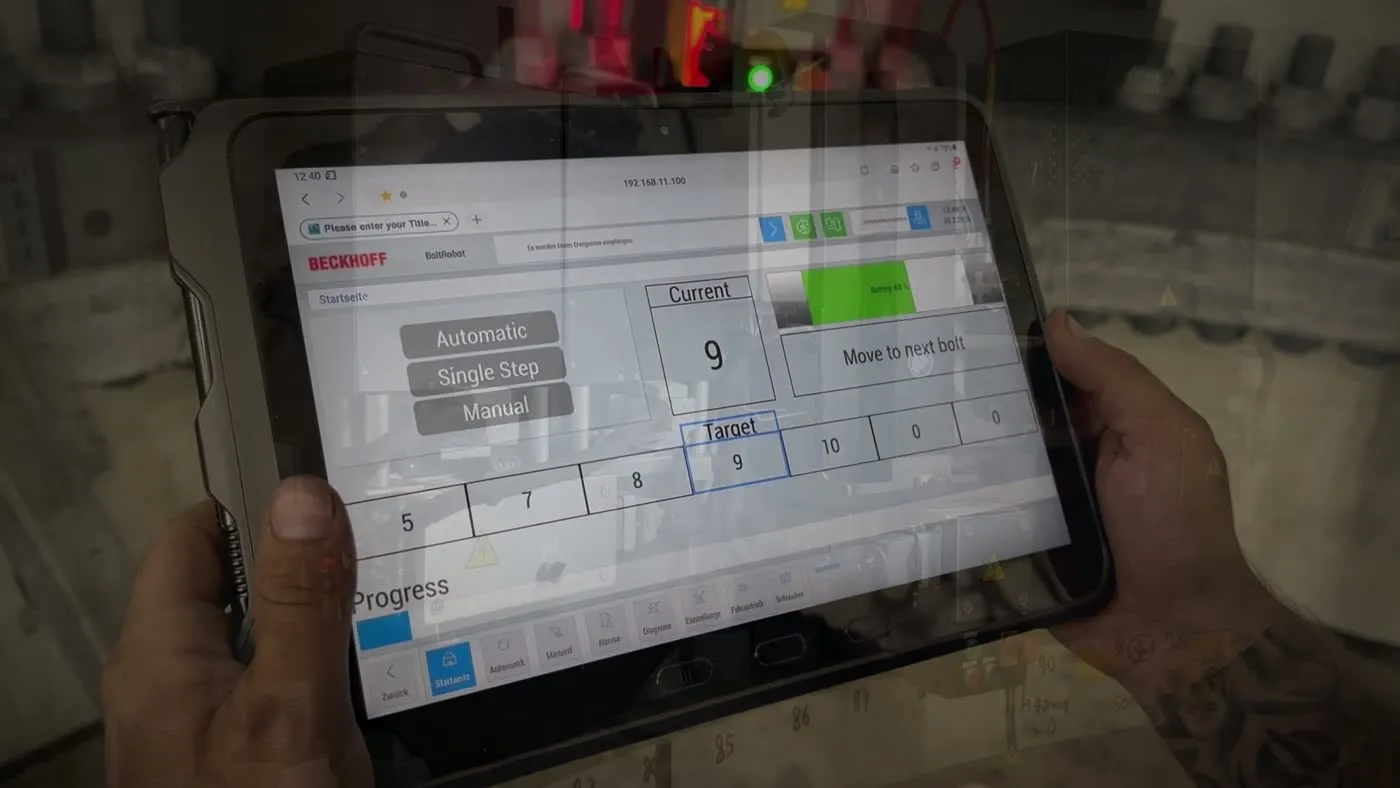
From a real offshore campaign
Bolt replacement, offshore wind farm, 2026
Tower connection flanges with 118 × M72 10.9 stud bolts, tensioned at 1,750 bar (2,725 kN) with Atlas Copco SmartTensioner tools.
Example charts from a flange report
Final accepted reading for each of the 110 bolts on one flange, drawn from the AutoBolt export.
Extract from a flange report
One line per pull, straight from the AutoBolt export. Pressure on two sensor channels, turn of the nut and residual torque.
| Bolt | Pull | Status | Time | Pressure A (bar) | Pressure B (bar) | Turn of nut (°) | Torque (Nm) |
|---|---|---|---|---|---|---|---|
| 1 | 1 | OK | 10:44:59 | 1,871.1 | 1,864.0 | 3.47 | 52.0 |
| 2 | 1 | OK | 10:45:43 | 1,853.3 | 1,913.6 | 1.82 | 46.2 |
| 3 | 1 | OK | 10:46:20 | 1,851.1 | 1,846.7 | 4.91 | 43.4 |
| 4 | 1 | OK | 10:46:59 | 1,842.2 | 1,817.2 | 0.76 | 47.3 |
| 5 | 1 | OK | 11:03:25 | 1,755.5 | 1,812.7 | 5.03 | 49.1 |
| 6 | 1 | OK | 11:04:03 | 1,806.6 | 1,851.6 | 1.56 | 51.9 |
What each report contains
- Executive summary: bolts tightened by AutoBolt, first-pull acceptance, final acceptance and process time
- Test parameters, equipment and acceptance criteria
- Tightening pattern, round by round
- Charts: hydraulic pressure, turn of the nut, residual torque and pulls per bolt
- Actual tightening path and elapsed time around the flange
- Exceptions and nonconformance register with corrective actions
- Detailed data — one line per pull for every bolt
"RESULT: All 118 bolts on this flange were successfully tensioned to the specified acceptance criteria (final acceptance 100%)."